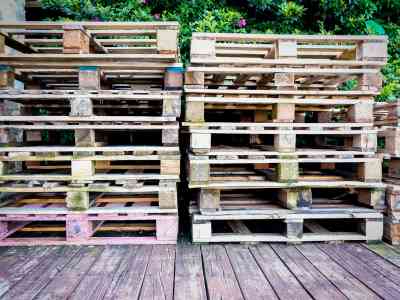
In the global supply chain, the safety and integrity of shipments are paramount. An often overlooked, yet crucial component of this process is the pallet. Pallets not only support goods during transit but also ensure that products reach their destination in optimal condition. Among the various types of pallets available, heat-treated pallets stand out as an excellent choice for safe shipping. This article delves into the benefits of using heat-treated pallets and why they are preferred for secure and efficient logistics.
Understanding Heat-Treated Pallets
Heat-treated pallets undergo a specific process where they are heated to a core temperature of 56 degrees Celsius for a minimum of 30 minutes. This process is designed to eliminate pests and pathogens that may reside in the wood. The result is a pallet that is more robust and compliant with international shipping standards, especially the ISPM-15 regulations.
Key Benefits of Heat-Treated Pallets
- Pest Control: The heat treatment process eradicates insects and larvae, preventing infestations during shipping and storage.
- Durability: Heat-treated pallets are less susceptible to mold and decay, ensuring a longer lifespan compared to untreated pallets.
- Compliance: They meet international standards, allowing for hassle-free shipping across borders. This compliance is crucial for companies engaged in global trade.
Environmental and Economic Advantages
Beyond safety, heat-treated pallets offer significant environmental and economic benefits:
- Eco-Friendly: Unlike chemical treatments, heat treatment leaves no toxic residues, making it a more environmentally friendly option.
- Cost-Effective: Although initially more expensive, the longevity and durability of heat-treated pallets can lead to cost savings in the long run. Discover expert strategies here.
- Reusability: Due to their increased durability, these pallets can be reused multiple times, reducing the need for constant replacements.
Applications in Various Industries
Heat-treated pallets are versatile and suitable for a wide range of industries.
- Food and Beverage: Ensures that shipments remain free from contamination, a critical requirement in this sector.
- Pharmaceuticals: Provides a sterile platform for transporting sensitive goods.
- Manufacturing: Offers reliable support for heavy and bulky items, ensuring safe transit. Find out more about this approach.
Conclusion: Making an Informed Choice
Choosing the right pallet for shipping needs is crucial for the success of any business involved in logistics. Heat-treated pallets offer a myriad of benefits, from enhanced safety and compliance to economic and environmental advantages. By opting for these pallets, businesses can ensure that their shipments are protected, compliant with international regulations, and cost-effective in the long run. For more insights and detailed information, explore advanced guides and tips available online. Making an informed choice about pallet selection can significantly enhance logistics efficiency and sustainability.